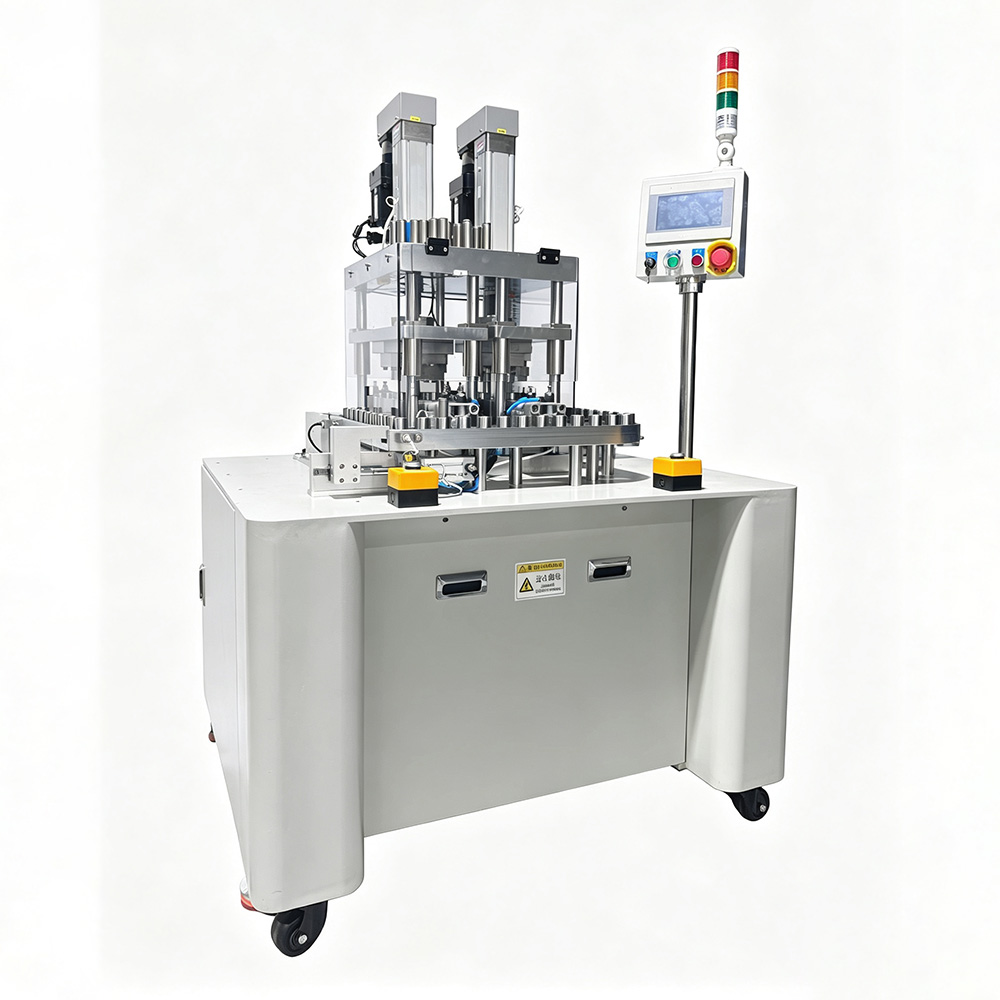
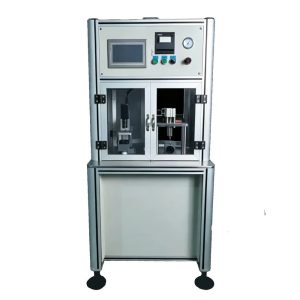
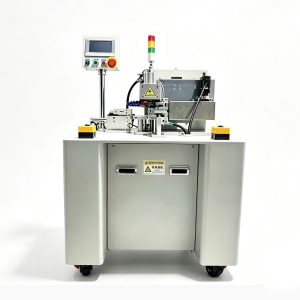
Equipment Description
Working principle: a servo transmission mechanism produces intermittent motion in the equipment. The machine uses a copper-bush guided seat combined with a high-precision, high-frequency guide rod to generate the large pressing force needed to compress the battery can and cap to the dimensions required by the process, thereby achieving battery sealing. Performance features: integrated electromechanical design, fully automatic PLC control, low energy consumption, low cost, high efficiency, high precision, convenient maintenance, and low failure rate.
Basic Configuration
| No. |
Component |
Description |
| 1 |
Servo Section (A) |
Servo driving a precision planetary reducer; positioning guide post performs high-performance up/down reciprocating motion via servo; full-stroke mold positioning; low noise; upper-mold descent at low speed (constant pressure); production efficiency controlled at 25–30 ppm; touch-screen manual fine adjustment for intelligent human-machine dialogue. |
| 2 |
Feed Section (B) |
Extra-long conveyor with increased load quantity; a row of magnets added to the feed-trough base plate; German NEY bearings for smooth feeding. |
| 3 |
Pushing Section (C) |
Smart inductor for close-range sensing of battery-in-place; dual-axis positioning with single-cylinder U-type pusher; pushes the cell to pre-press the cap; pre-seal mold includes cap-pressing function; first-, second-, third-, and fourth-seal actions completed in one interlocked cycle. |
| 4 |
Mold-Closing Section (D) |
Air-pressure-driven AirTAC cylinder actuates a bidirectional mold seat for cyclic mold closing to complete continuous sealing; moving mold seat of oil steel, heat-treated and precision-machined, wear-/corrosion-/heat-resistant; precision mold-closing alignment; upper mold will not descend until mold closing is complete (protects the lower mold); lower-mold positioning flatness 0.4 mm. |
| 5 |
Mold Section (E) |
Upper mold: first, second, third, and fourth seals all use four-seal form; mold center axis matches the mold-seat tapered center hole; mold seat is pin-positioned on the mold connecting plate; upper/lower molds made of wear-resistant oil steel with high precision; high-precision mold bushing of SKD-11-class material, hardness ≥ HRC 55; first/second/third/fourth-seal upper molds fixed with semi-circular lock blocks on top; molds have a usage-count function; non-human-damage single-mold service life reaches over 1,000,000 cells. |
| 6 |
Discharge Section (F) |
Unloading mechanism automatically discharges cells to the output trough; a motor-driven belt transfers finished batteries; left-side discharge; discharge and feed (right-side) handled by a single operator. |
| 7 |
Electrical Section (G) |
Manual mode first for mold trial to meet process requirements, then switch to automatic mode; rigorous, convenient, and safe Mitsubishi electrical program with full-process product monitoring; multiple inductive switches; safety light curtain; automatic alarm on abnormality; automatic stop on improper operation; PLC output switching via solid-state relays controlling solenoid valves; emergency-stop provided for on-demand immediate stop. |
| 8 |
Key Components |
AirTAC cylinders; Mitsubishi / Huichuan electrical control system; upper-frame touch-screen micro-adjust control; SMC sensor; Omron power supply; safety protection device; upper pressure plate opens/closes with protection; first/second/third/fourth-seal mold material DC53; fourth seal is squat-seal; base plate thickened by 10 mm to 49 mm with stiffening ribs; frame column changed to side plate; servo with planetary reducer; guide-post guidance; sound-absorbing cotton applied around lower-frame door; front feed取消了 two pushers for direct feeding. |
Technical Parameters
| No. |
Parameter |
Value |
Remarks |
| 1 |
Sealing total height |
0.1 mm |
|
| 2 |
Sealing edge height |
0.05 mm |
|
| 3 |
Post-sealing diameter |
0.05 mm |
|
| 4 |
Post-sealing diameter concentricity |
0.05 mm |
|
| 5 |
Applicable steel-can diameter |
15–81 mm |
|
| 6 |
Applicable height range |
41–0.1 mm |
|
| 7 |
Post-sealing no flaring/ovality error |
0.02 mm |
|
| 8 |
Lower-mold installation flatness |
0.02 mm |
|
| 9 |
Upper-mold height error |
0.01 mm |
|
| 10 |
Upper-mold diameter error |
0.01 mm |
|
| 11 |
Applicable steel-can range |
18650 |
|
| 12 |
Applicable height range |
652 mm |
|
| 13 |
Rated voltage |
220 V / 50 Hz |
|
| 14 |
Rated power |
2.5 kW |
|
| 15 |
Working air pressure |
5–6 kgf/cm² |
|
| 16 |
Efficiency |
25–30 pcs/min |
|
| 17 |
Overall dimensions (L×W×H) |
1200 × 1919 × 1900 mm |
|
| 18 |
Equipment weight |
1000 kg |
|
| 19 |
Included tooling |
1 set of molds supplied with the machine |
|